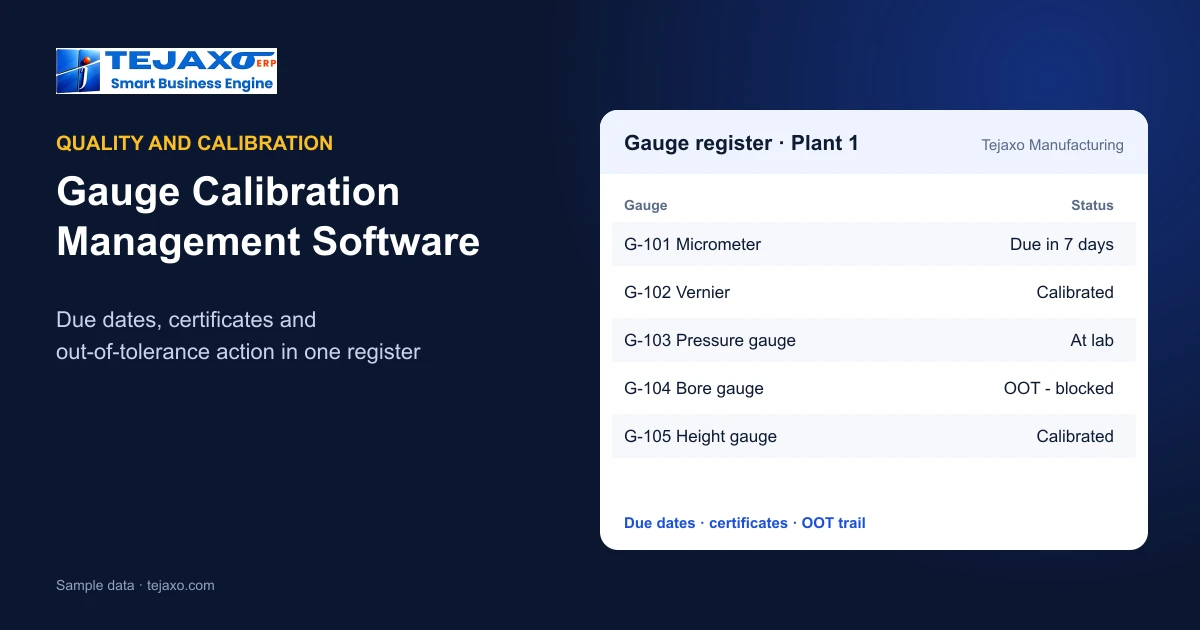
Gauge calibration management software is a system that keeps a register of every gauge and instrument, schedules calibration due dates, stores certificates, and records what was done when a gauge is found out of tolerance. For a manufacturer, the real value is simple: no gauge is used past its due date, and any auditor can see the full history of any instrument in a few clicks. This guide explains what to look for, how it maps to common quality standards, and how to roll it out in a plant.
What gauge calibration management software actually does
Every plant that measures its product owns vernier calipers, micrometers, pressure gauges, thermometers, torque tools, go/no-go gauges and more. Each one needs to be checked against a traceable reference at a planned interval. Calibration management software turns that routine into a controlled process.
At a minimum it should handle:
- A gauge master with a unique ID, type, range, least count, location, owner and status.
- Calibration schedules that generate a due list automatically from the last calibration date and the interval.
- Calibration records with readings, acceptance criteria, result and the person who performed it.
- Certificate storage linked to the gauge, so no one hunts through files.
- Out-of-tolerance (OOT) handling with a documented impact assessment.
- Status control so that an overdue or rejected gauge is clearly marked as not for use.
More advanced tools also add measurement system analysis (MSA) studies such as Gauge R&R, barcode or QR tagging, and multi-plant views. Whether you need all of these depends on your customers and your quality system.
Why Excel registers and paper files fail at audit time
Most small and mid-sized plants in Faridabad, Gurgaon, Manesar and Noida start with an Excel register. It works while there are 50 gauges and one careful person. It breaks as the plant grows.
- Missed due dates. Nobody opens the sheet on the day a gauge expires, so it stays in use on the shop floor.
- Lost or mismatched certificates. The certificate sits in a file, a mailbox or a vendor’s WhatsApp message.
- No impact trace. When a gauge fails its check, nobody can quickly say which lots were measured with it since the last good calibration.
- Version confusion. Two plants keep two sheets with different formats and different interval rules.
- Weak access control. Anyone can edit a date, and there is no history of who changed what.
Auditors rarely fault the idea of a spreadsheet. They fault the lack of control around it. Software gives you the control without adding clerical work.
Standards and what auditors look for
The table below is a practical map between common quality-system expectations and software features. It is a working guide, not a legal reading. Always confirm the exact clause wording and your customer-specific requirements against the current edition of each standard.
| Typical expectation | Where it usually appears | What the software should provide |
|---|---|---|
| Measuring equipment is calibrated or verified against traceable standards at planned intervals | ISO 9001 (monitoring and measuring resources) | Schedules, interval rules, linked certificates with traceability reference |
| Calibration records are retained | ISO 9001, IATF 16949 | Permanent history per gauge, with date, result and performer |
| Action when equipment is found out of tolerance, including impact on earlier measurements | ISO 9001, IATF 16949 | OOT workflow with impact assessment and sign-off |
| Measurement system analysis for critical characteristics | IATF 16949 (automotive supply chain) | Gauge R&R and related study records linked to the gauge |
| Competence and traceability of calibration providers | ISO/IEC 17025 for labs; NABL accreditation in India | Approved vendor list, certificate scope check, validity tracking |
| Data integrity for regulated environments | Pharma and GxP practice | User rights, audit trail, controlled edits |
If your customers are automotive Tier-1 or Tier-2 companies, expect questions on OOT impact assessment and MSA during their supplier audits. If you serve pharmaceutical customers, expect questions on audit trails and controlled records. Our page on ERP for the automobile and auto components industry explains how quality records fit into the wider production flow.
Core features checklist for gauge calibration management software
Use this checklist when you compare tools. Mark each line as must-have, nice-to-have or not needed for your plant.
| Area | What to ask | Why it matters |
|---|---|---|
| Gauge master | Can we capture type, range, least count, location and custodian? | Clean data is the base for every report |
| Scheduling | Does it generate due lists and handle different intervals per gauge type? | Prevents gauges from running past due |
| Alerts | Who is notified before and after the due date, and on which channel? | A due list nobody sees is the same as no list |
| Certificates | Can we attach and search certificates by gauge and vendor? | Audit evidence in seconds |
| OOT workflow | Does it force an impact assessment before the gauge is released? | Shows that you acted on the failure |
| Status control | Is a gauge visibly blocked when overdue or rejected? | Protects the shop floor |
| Tagging | Can we use a barcode or QR label on each gauge? | Fast lookup at the point of use |
| Vendors | Can we track outside calibration labs and their certificate validity? | Traceability depends on the lab |
| Access and history | Is there user-wise access and an audit trail? | Prevents silent edits |
| Reports | Due list, overdue list, history card, OOT list, vendor-wise status | What the auditor will ask to see |
| Multi-plant | Can head office see all plants on one screen? | Consistent rules across locations |
Out-of-tolerance handling: a worked example
OOT handling is where many registers are weakest, so it deserves a worked example. The numbers below are invented samples for illustration.
Tejaxo Manufacturing uses a micrometer, Gauge ID G-101, to inspect Product A. The last good calibration was on 1 April. On 1 October the gauge is calibrated again and found reading outside its tolerance.
- Block the gauge. The system marks G-101 as rejected, and it no longer appears as available for issue.
- Find the exposure window. The period between the last good calibration (1 April) and the failed check (1 October) is the window in which measurements may be wrong.
- List what was measured. Inspection records that used G-101 in that window are pulled up, with the lots and dates.
- Judge the impact. The quality team checks the size and direction of the error against the product tolerance. Some lots may be unaffected, others may need re-inspection with a good gauge.
- Decide and record. Re-inspect, hold, recall or accept with justification. The decision, the person and the date are stored on the OOT record.
- Close the loop. The gauge is repaired or replaced, recalibrated and released only after approval.
The difficulty in Excel is step 3. Linking inspection records to the gauge used needs a system that holds both together. This is one reason plants running a connected ERP have an advantage over those running a standalone register. For defect and quality cost analysis after such events, see our article on PPM, defect Pareto and cost of poor quality.
Outsourced calibration and certificate control
Many NCR plants send gauges to external laboratories, especially for pressure, temperature, mass and flow instruments. In India, the usual route to traceable results is a laboratory accredited by NABL against ISO/IEC 17025. Your system should therefore treat the calibration vendor as part of the record, not an afterthought.
- Keep an approved calibration vendor list with their accreditation validity.
- Check that the scope on the certificate covers the range and parameter of your gauge.
- Record dispatch and return dates so that a gauge sent out is not shown as available.
- Attach the certificate to the gauge history as soon as it arrives, and review the stated error against your acceptance criteria before release.
Managing the vendor side with the same discipline you apply to purchase vendors helps. Tejaxo offers a vendor management portal that can serve as the base for document exchange with suppliers and service providers.
How Tejaxo handles calibration requests and tracking
Tejaxo’s service booking app covers calibration requests and tracking. A customer chooses the calibration type, such as electrical, temperature, pressure, mass or flow, and raises the request from the app. After that, each stage is visible: verification, quotation and the final calibration report.
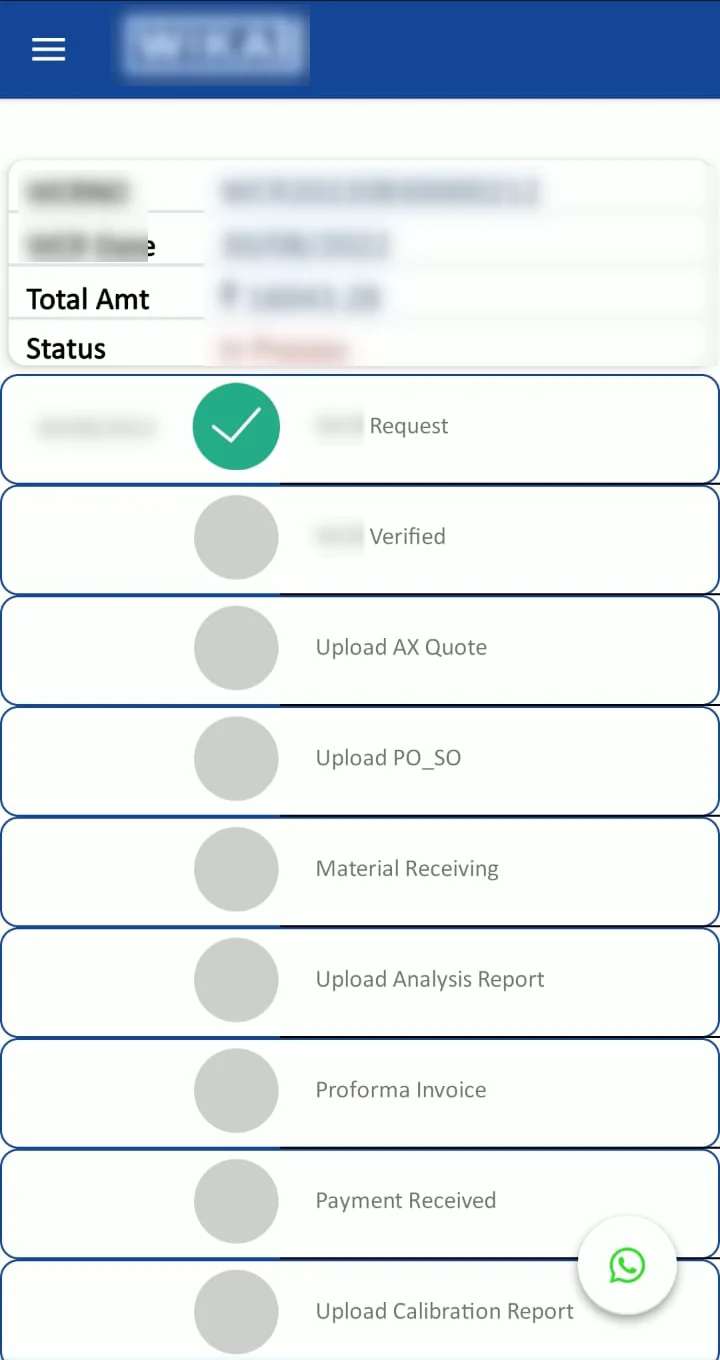
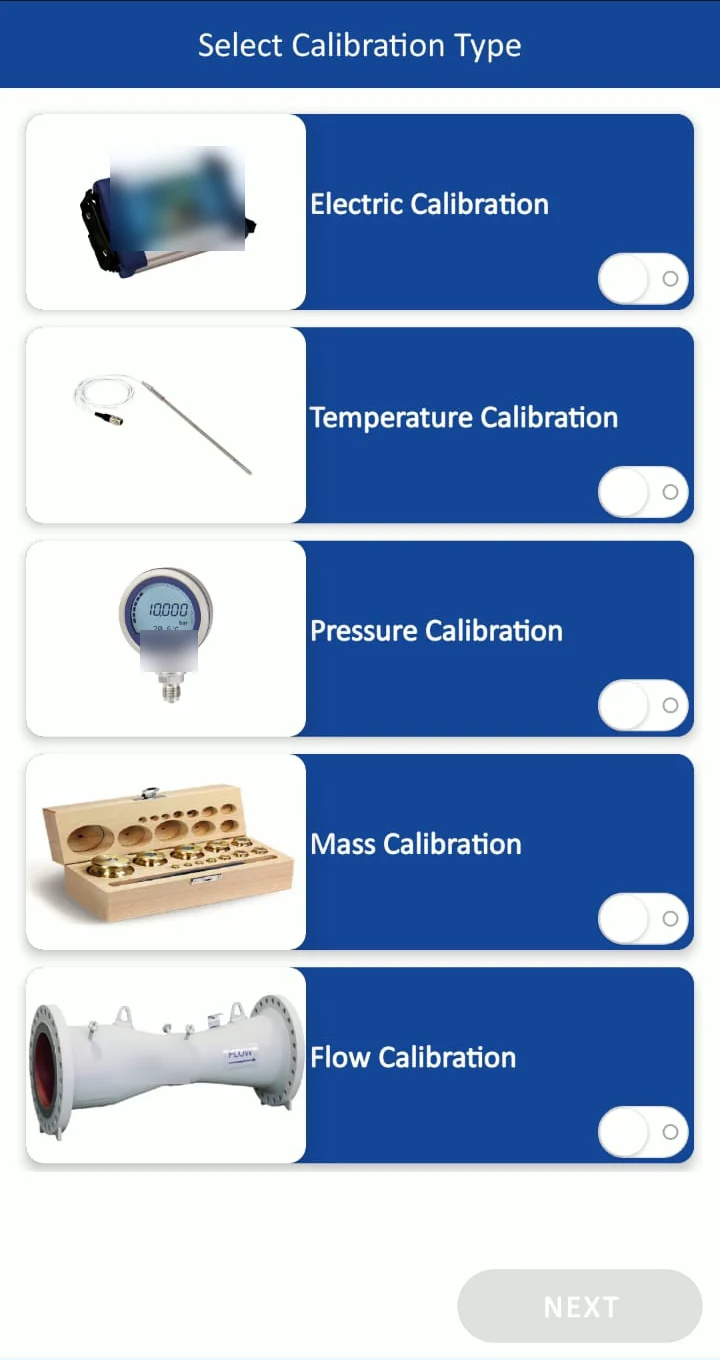
This is useful in two situations. If your plant is a calibration service provider, it gives your customers a clear view of where their instrument is. If your plant sends instruments to outside labs, the same stage-wise discipline gives you a model for tracking dispatch, quotation, calibration and report receipt.
You can read more on our page about the service management app for calibration and repair.
Standalone tool or part of your ERP?
A standalone calibration tool is simple to start with. Its weakness is that it sits apart from purchase, stores, production and quality. Gauges are bought through purchase, issued from stores, used in production inspection and discarded through asset records. When those steps live in different systems, someone has to reconcile them by hand.
| Point | Standalone tool | Connected to ERP |
|---|---|---|
| Start-up effort | Low | Depends on the ERP already in use |
| Link to inspection records | Manual | Possible through shared data |
| Purchase and vendor data | Entered again | Shared with the purchase module |
| Alerts to owners | Tool-specific | Same alert channel as other approvals |
| Management reports | Separate | Part of the same dashboards |
If you already run SAP or Microsoft Dynamics, you do not need to replace it. Tejaxo extends your existing ERP rather than replacing it. Tejaxo ERP itself is an automated manufacturing ERP with WhatsApp alerts and approvals, a live owner view and a large set of ready reports, so calibration follow-up can use the same alert path your managers already use. Ask during a demo how a calibration register would be set up for your plant, as requirements differ from one plant to another.
Implementation steps for a plant in NCR
- Take a physical inventory. Walk the shop floor, tool crib and lab. List every gauge, including those in personal custody.
- Clean the master data. Assign unique IDs, remove duplicates, and mark gauges that are retired or lost.
- Define intervals. Set a starting interval per gauge type based on usage, manufacturer advice and customer requirements. Review it later using history.
- Tag each gauge. Use a durable barcode or QR label and a visible calibration status label.
- Load history. Bring in the last calibration date and certificate for each gauge. Our guide on ERP data migration of masters and opening balances covers how to approach this safely.
- Set roles. Decide who can create records, who approves OOT decisions and who can release gauges.
- Train and go live. Start with one area, such as the inspection lab, then extend to the shop floor.
- Review monthly. Check the overdue list, OOT list and vendor turnaround at your regular quality review.
Questions to ask any vendor before you buy
- How does the system stop an overdue gauge from being used, rather than just reporting it?
- Can we link OOT events to the inspection records made with that gauge?
- How are certificates stored, searched and protected from edits?
- Can it support our customers’ audit formats and our own plant naming?
- Is it cloud, on-premise or hybrid, and where is our data kept?
- What support is available on-site and remotely for plants in our area?
- How will our existing Excel register be imported?
Be wary of tools that look good in a demo but cannot show a real OOT trace. Ask to see that scenario with your own sample data.
Next step: talk to Tejaxo
Tejaxo Technologies has been in business since 2017 and supports manufacturers across India on-site and remotely, including plants across Delhi NCR such as Faridabad. If you want to move your gauge register from Excel to a controlled system, or connect calibration to your wider ERP, book a free consultation and we will review your current process, your audit expectations and a practical roll-out plan.
Frequently asked questions
What is gauge calibration management software?
It is software that keeps a register of all gauges and measuring instruments, schedules their calibration, stores certificates and records results. It also controls out-of-tolerance events by forcing an impact assessment and blocking unfit gauges. The goal is to ensure no instrument is used past its due date and to provide audit-ready history on demand.
Which features matter most in calibration software for a factory?
The most important features are a clean gauge master, automatic due lists, alerts before expiry, certificate storage, an out-of-tolerance workflow with impact assessment, and visible status control for overdue gauges. Vendor tracking, barcode or QR tagging, user-wise access with an audit trail, and due and history reports are also valuable for audits.
How does it help with ISO 9001 and IATF 16949 audits?
These standards expect measuring equipment to be calibrated against traceable references, records to be retained, and action to be taken when equipment is found out of tolerance. The software keeps schedules, certificates and history in one place and records the impact assessment, so you can show evidence quickly. Always check exact clause wording and customer requirements.
Is Excel enough to manage gauge calibration?
Excel can work for a very small gauge count and one careful owner. It struggles as the plant grows because it gives no automatic alerts, no edit history, weak certificate control and no link to inspection records. These gaps cause missed due dates and weak out-of-tolerance tracing, which auditors commonly question.
How do we handle outside calibration labs and NABL certificates?
Keep an approved vendor list with accreditation validity, check that the certificate scope covers your gauge's range and parameter, and record dispatch and return dates so a gauge sent out is not shown as available. Attach the certificate to the gauge history on arrival and review the stated error against your acceptance criteria before release.
Should calibration software be connected to our ERP?
Connecting it helps because gauges move through purchase, stores, inspection and asset records. Shared data lets you trace which inspections used a failed gauge and reuse vendor details and alerts. A standalone tool is quicker to start, but it needs manual reconciliation. If you use SAP or Dynamics, extend it rather than replace it.