
Paper is the largest cost in a corrugated box, and the strength of the box depends on the paper inside it. Yet in many plants reels are unloaded, stacked and used on the strength of the supplier’s challan alone. When a box later fails a burst or compression check at the customer, nobody can say which reel it came from. Reel inward inspection fixes that: every reel is tested and recorded against the goods receipt before it is accepted. This guide explains what to test, how to read the results and how to record it reel by reel in an ERP.
Why test every reel
- Paper sets the box strength. A liner below its GSM or bursting factor makes a weaker board, however well the corrugator runs.
- Problems found later cost more. A weak reel found at the gate is a supplier return; found in a failed box, it is a rejected order.
- Supplier performance becomes visible. Reel-wise results show which supplier and which grade keep missing the order specification.
- Traceability starts at the reel. If the reel number is recorded at receipt, a box can be traced back to the paper it was made from.
What is tested
- Reel number and weight: the identity of the reel and its actual weight, against the weight on the supplier’s documents.
- Deckle: the reel width, which must suit the corrugator and the deckle in the Process Plan.
- GSM: grams per square metre, measured from samples and averaged, against the GSM ordered.
- Burst strength: the pressure at which the paper bursts, usually measured more than once and averaged.
- Bursting factor (BF): burst strength related to GSM, so papers of different weights can be compared. A common working formula is BF = burst strength (kg/cm²) x 1,000 / GSM.
- RCT (ring crush test): the edgewise compression strength of the paper, which drives the stacking strength of the finished box.
- Result: accept or reject, with the accepted and rejected weight.
How GSM is checked at the gate
GSM is simply weight per area. Cut a sample of known area from the reel – for example a 10 x 10 cm square, which is 0.01 square metres – and weigh it on a precise balance. If the sample weighs 1.50 g, the paper is 1.50 / 0.01 = 150 GSM. Take more than one sample across the width of the reel and record each observation as well as the average, because paper can vary from edge to centre. The same discipline applies to burst: several readings, each recorded, and the average used for the bursting factor.
Worked example: two reels from one receipt
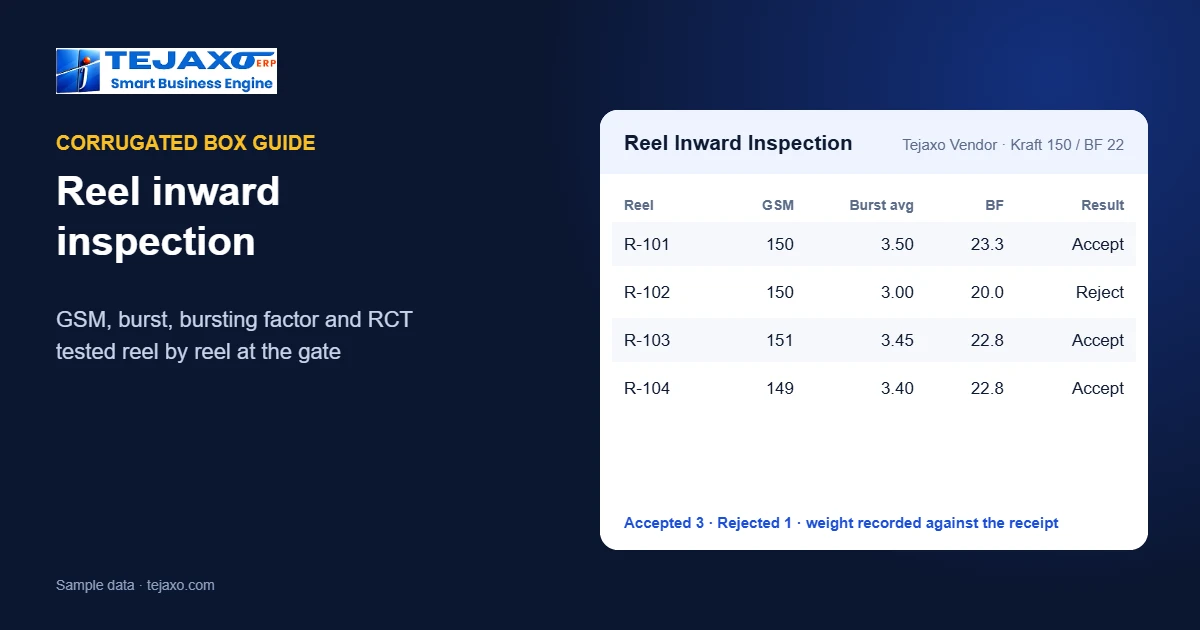
Tejaxo Manufacturing receives kraft paper from Tejaxo Vendor ordered at 150 GSM and BF 22 (sample numbers). Two reels are tested:
| Reel | GSM | Burst avg | BF | Result |
|---|---|---|---|---|
| R-101 | 150 | 3.50 | 23.3 | Accept |
| R-102 | 150 | 3.00 | 20.0 | Reject |
Burst readings for R-101 were 3.4, 3.6 and 3.5 kg/cm² (average 3.50), giving a bursting factor of 3.50 x 1,000 / 150 = 23.3 – above the BF 22 ordered, so the reel is accepted. R-102 averaged 3.00 kg/cm², a bursting factor of 20.0, below specification, so it is rejected and its weight is recorded as rejected against the receipt. The supplier is informed with reel-wise figures rather than an argument about “weak paper”.
How it works in Tejaxo ERP
In Tejaxo ERP for packaging, reel inward inspection is a quality template linked to the goods receipt. The header picks up the receipt and supplier and holds the required BF, required GSM and paper grade, with the total, accepted and rejected quantity. The grid has one line per reel: reel number, reel weight, deckle size, GSM observations and average, burst readings and average, bursting factor, RCT, result, and accepted and rejected weight. Accepted reels go into stock batch-wise with their reel number, so they can be issued against a job and traced afterwards.
From the tested reel to the finished box
- Receipt and inspection: reels are tested and accepted or rejected against the goods receipt.
- Process Plan: the box design names the paper, GSM and BF for every layer – see how the paper weight of a corrugated box is calculated.
- Job Card and issue: the job’s paper request is issued from accepted stock, reel by reel.
- Stage-wise production: corrugation, printing, stitching and the other stages are recorded with good output, rejection and downtime by reason – see corrugated box production in ERP.
What happens to a rejected reel
A rejected reel should never reach the corrugator by accident. Record its rejected weight on the inspection against the goods receipt, keep it apart from accepted stock, and return it to the supplier with a purchase return and debit note, so the payable is reduced by exactly the weight rejected – see from gate entry to debit note. Over a few months, rejection by supplier and paper grade shows purchase where to place the next order.
Setting accept and reject limits
Every plant needs written limits before the first reel is tested. Agree with purchase and production what counts as acceptable for each paper grade – for example, how far below the ordered GSM or BF a reel may fall before it is rejected, and which readings must be taken on every reel and which on a sample. Keep the limits in the quality template rather than in the inspector’s memory, so every shift applies the same rule and the result can be defended to the supplier.
Reports worth watching every month
- Accepted vs rejected weight by supplier and paper grade, to see who consistently meets the specification.
- Reel and stock ageing, so old reels are used first and paper does not sit in the godown absorbing moisture.
- Issue vs production per job, to check that the paper issued from accepted stock matches what the job actually produced.
Common mistakes
- Testing only the first reel of a lot. One good reel says little about the rest; record every reel, even if some tests are on a sample.
- Recording averages only. Keep the individual readings – a wide spread is itself a warning sign.
- Not linking the test to the receipt. Without the link, rejected weight never reaches the supplier’s debit note.
- Losing the reel number after acceptance. Store and issue reels by number, or traceability ends at the gate.
- No feedback to purchase. Reel-wise rejection by supplier and grade should guide the next order.
Next step
See reel inward inspection, the Process Plan and stage-wise production on your own paper grades. Book a free demo, or try the free corrugated box calculator.
Frequently asked questions
What is checked when paper reels arrive at a corrugation plant?
Reel number and weight, deckle, GSM, burst strength (several readings and the average), bursting factor, RCT and the result, with the accepted and rejected weight recorded against the goods receipt.
How is bursting factor calculated?
A common working formula is BF = burst strength (kg/cm²) x 1,000 / GSM. For example, a 150 GSM paper bursting at 3.5 kg/cm² has a bursting factor of about 23.3.
What is RCT in paper testing?
The ring crush test measures the edgewise compression strength of the paper, which affects how much load a finished box can carry when stacked.
Why record every reel separately?
Because reels in one lot can differ. Reel-wise records let you reject only the weak reels, show the supplier exact figures and trace a failed box back to the paper it was made from.
Can reel inspection be linked to the goods receipt in an ERP?
Yes. In Tejaxo ERP the reel inward inspection is a quality template linked to the goods receipt, with required BF, GSM and grade in the header and one line per reel in the grid.
What happens to accepted reels?
They go into stock batch-wise with their reel number, are issued against job cards, and can be traced from the finished box back to the reel.